


 عربى

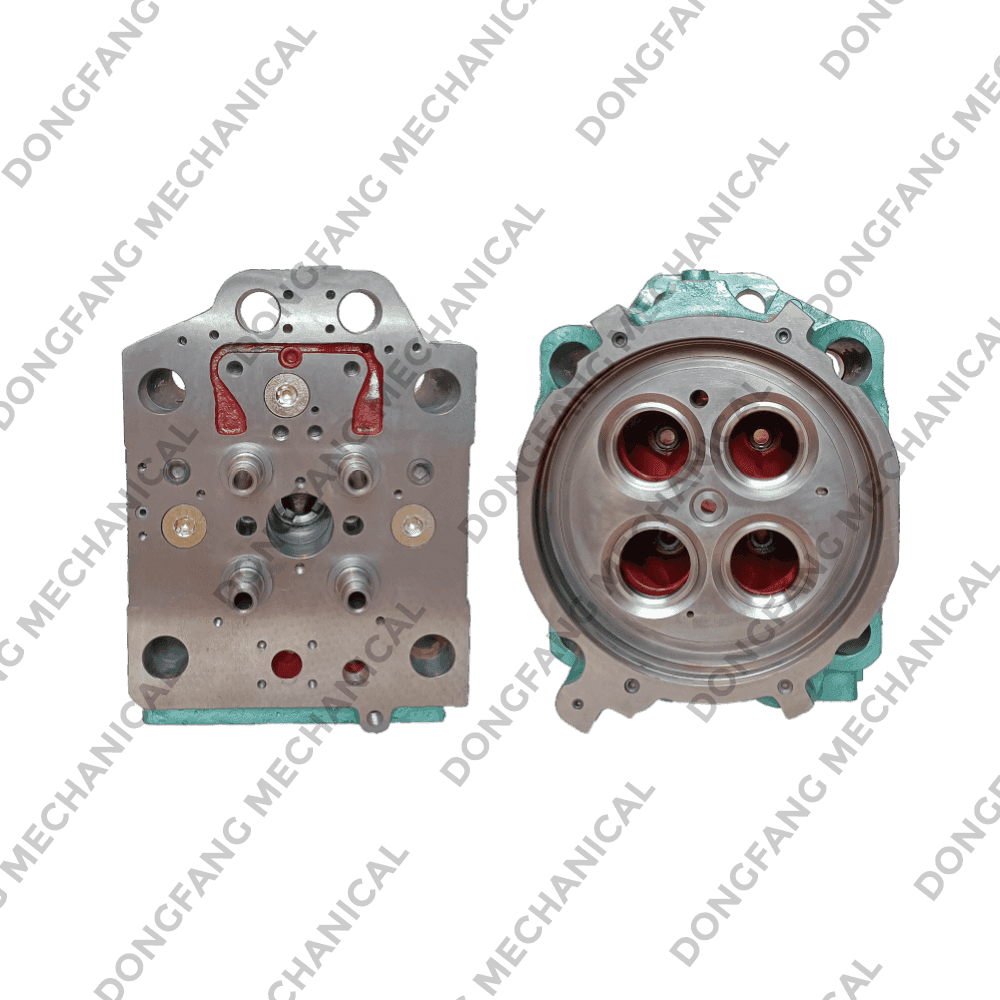
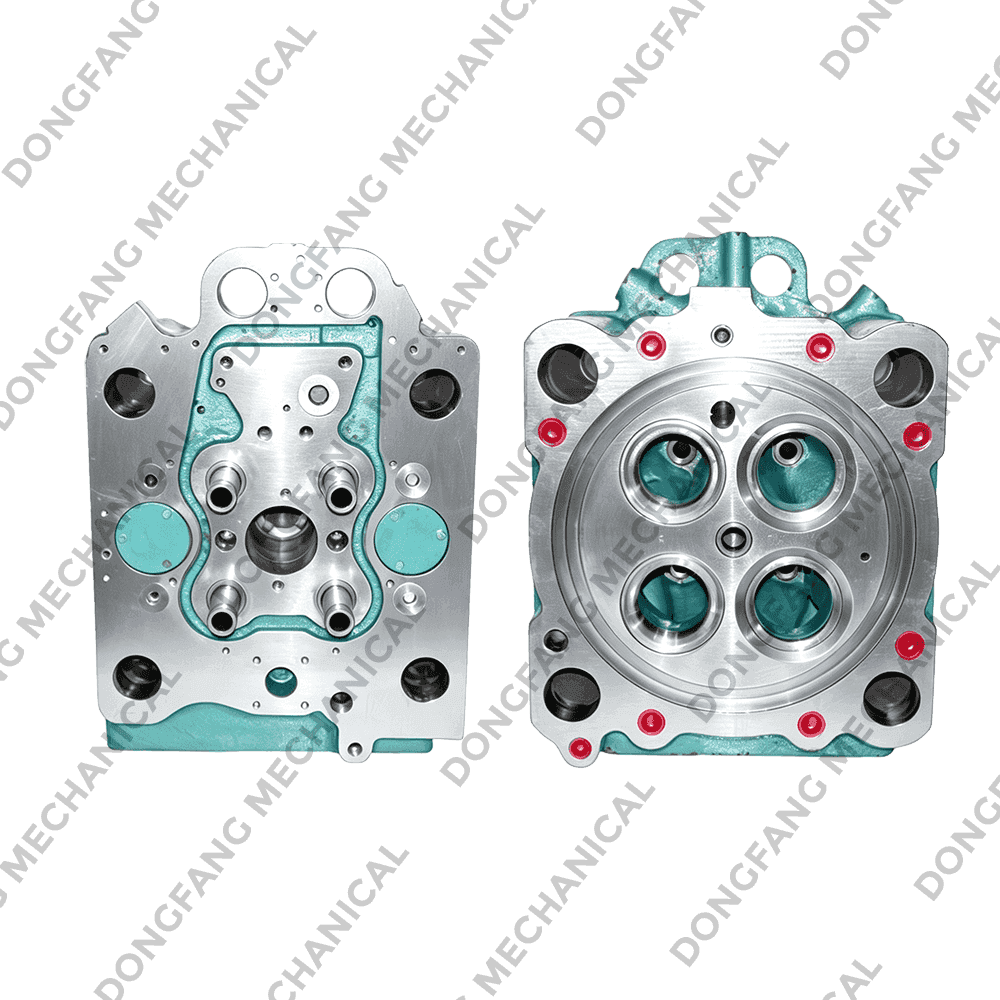
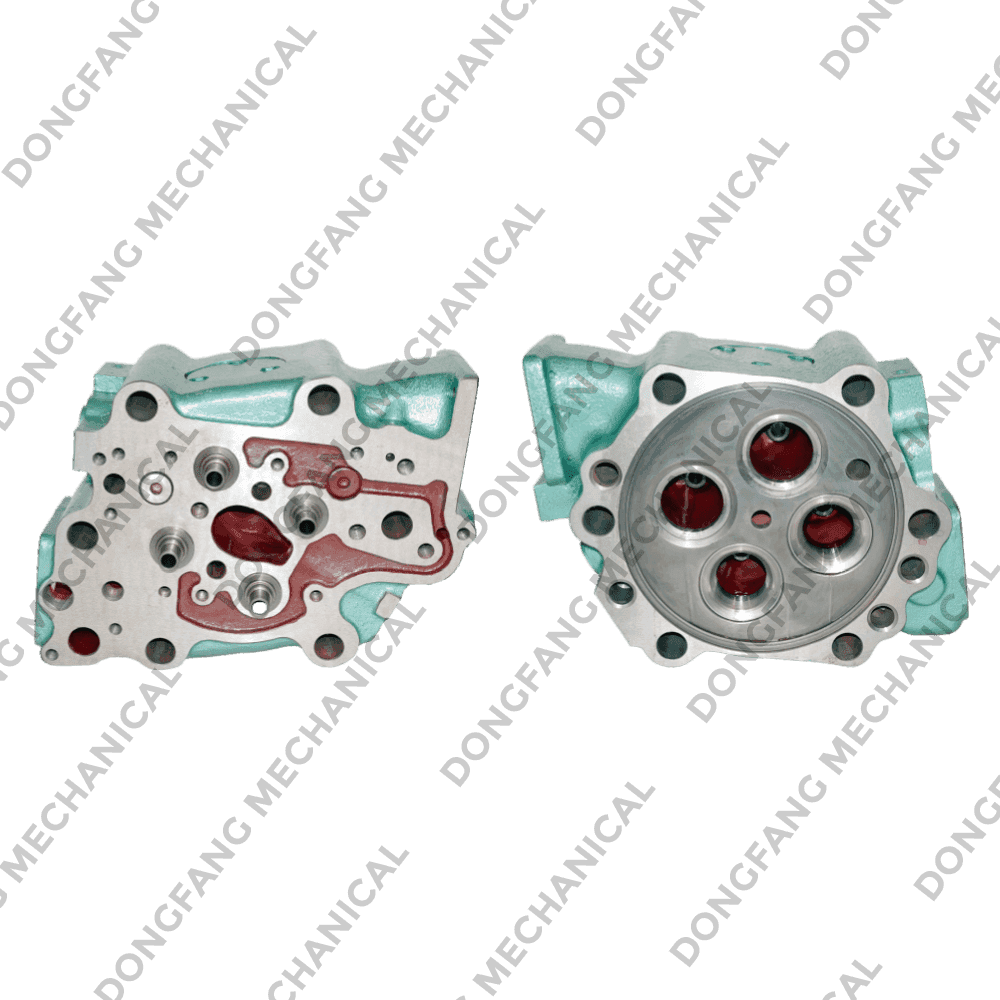
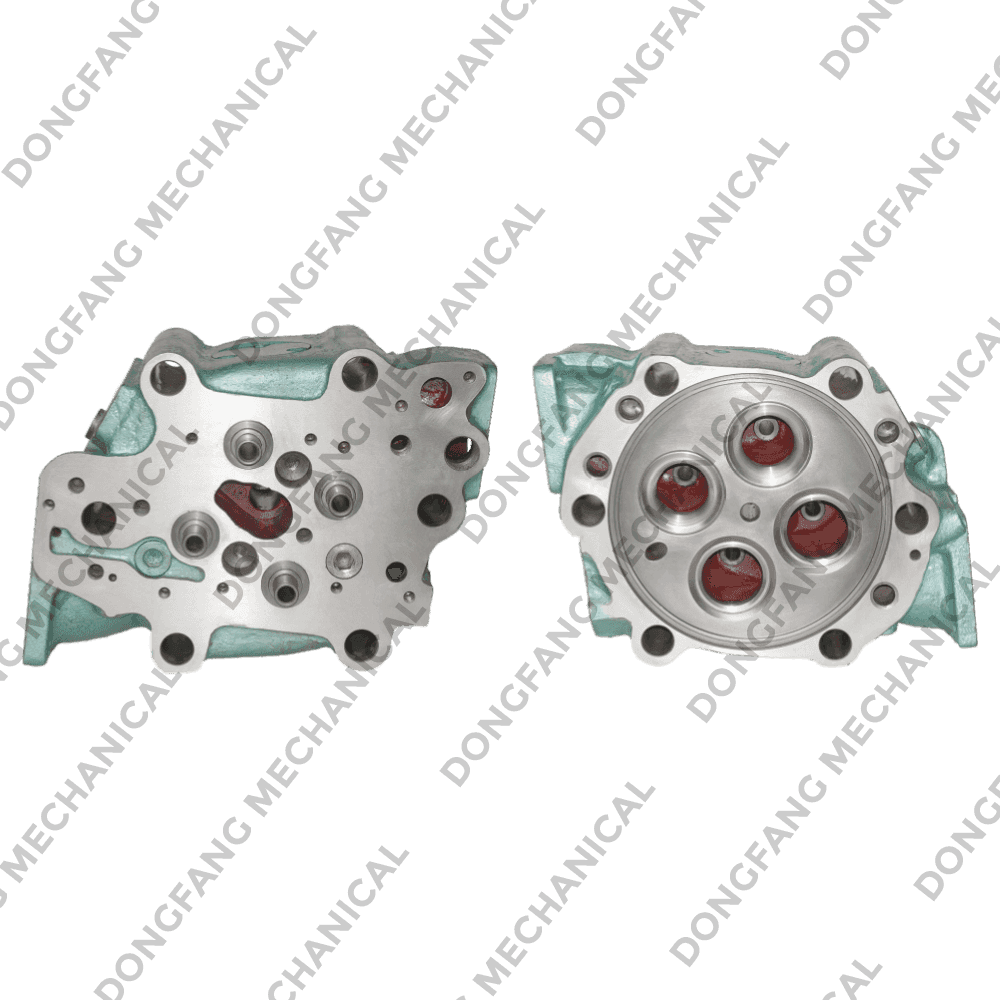
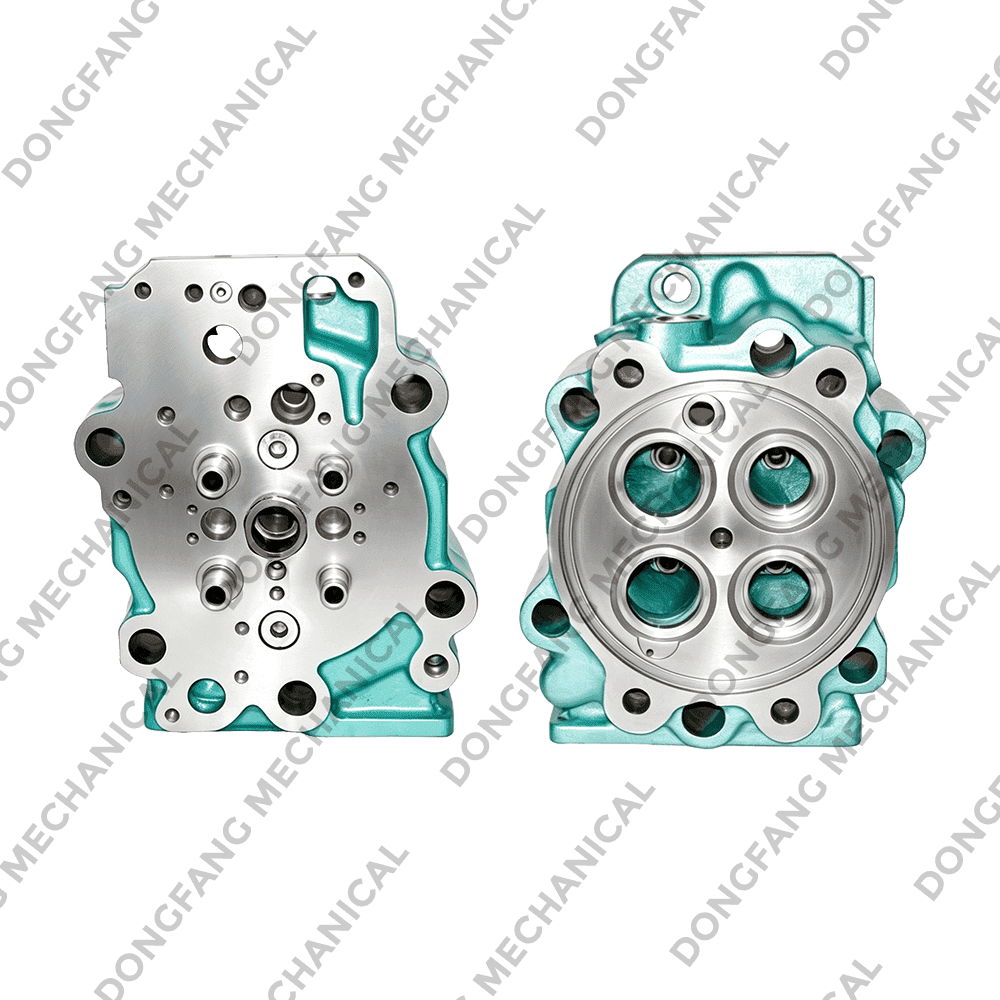
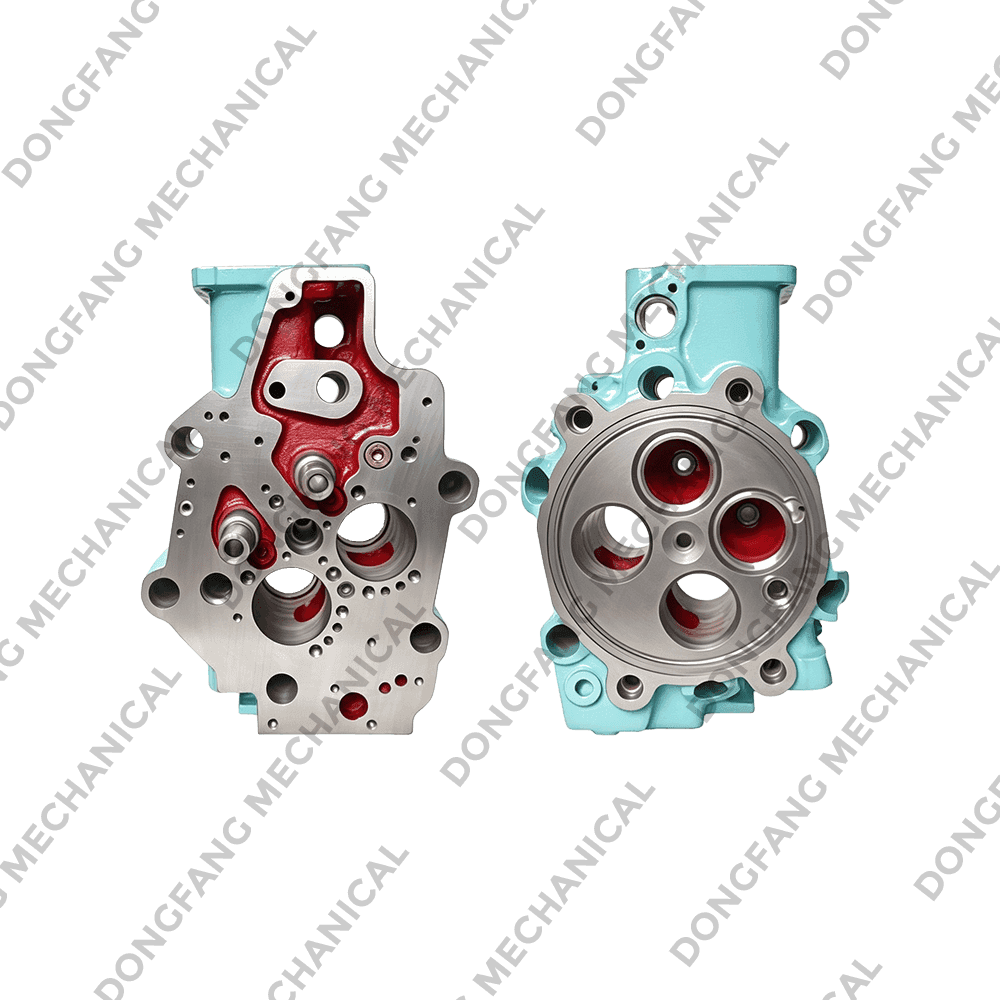
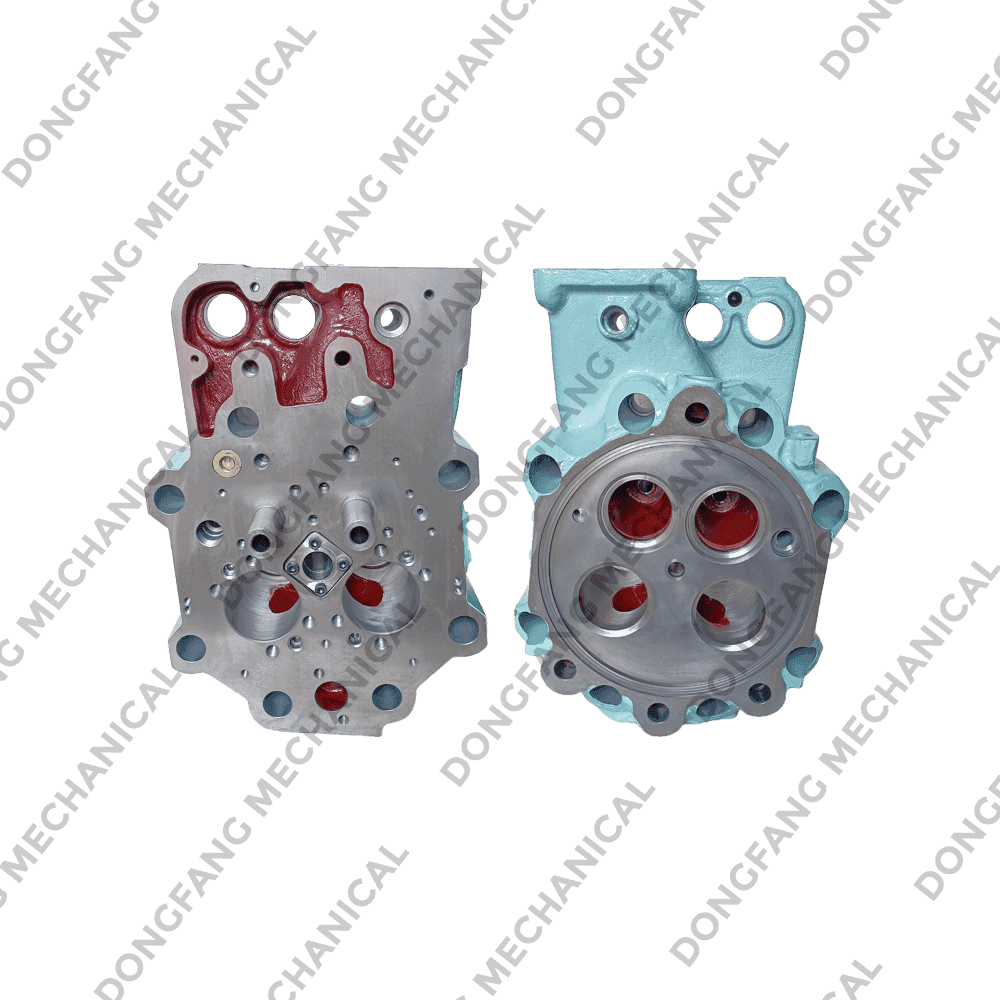
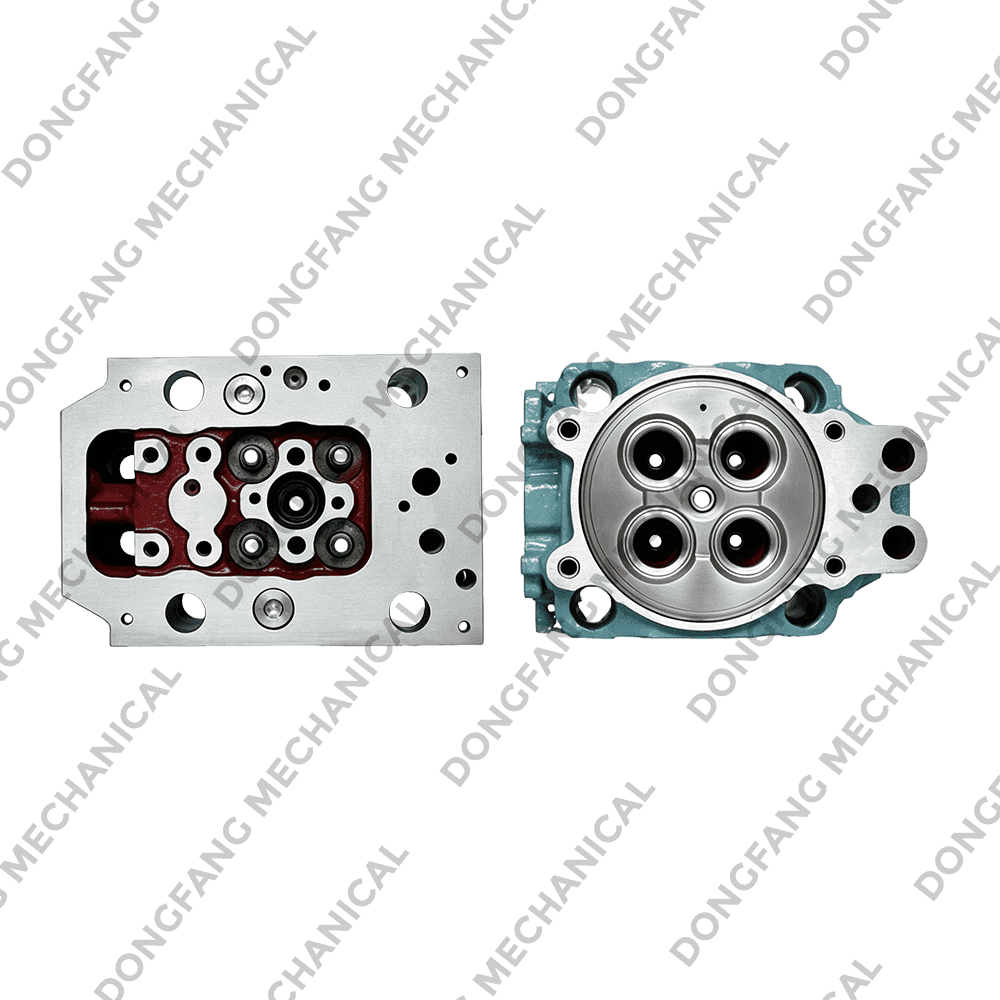
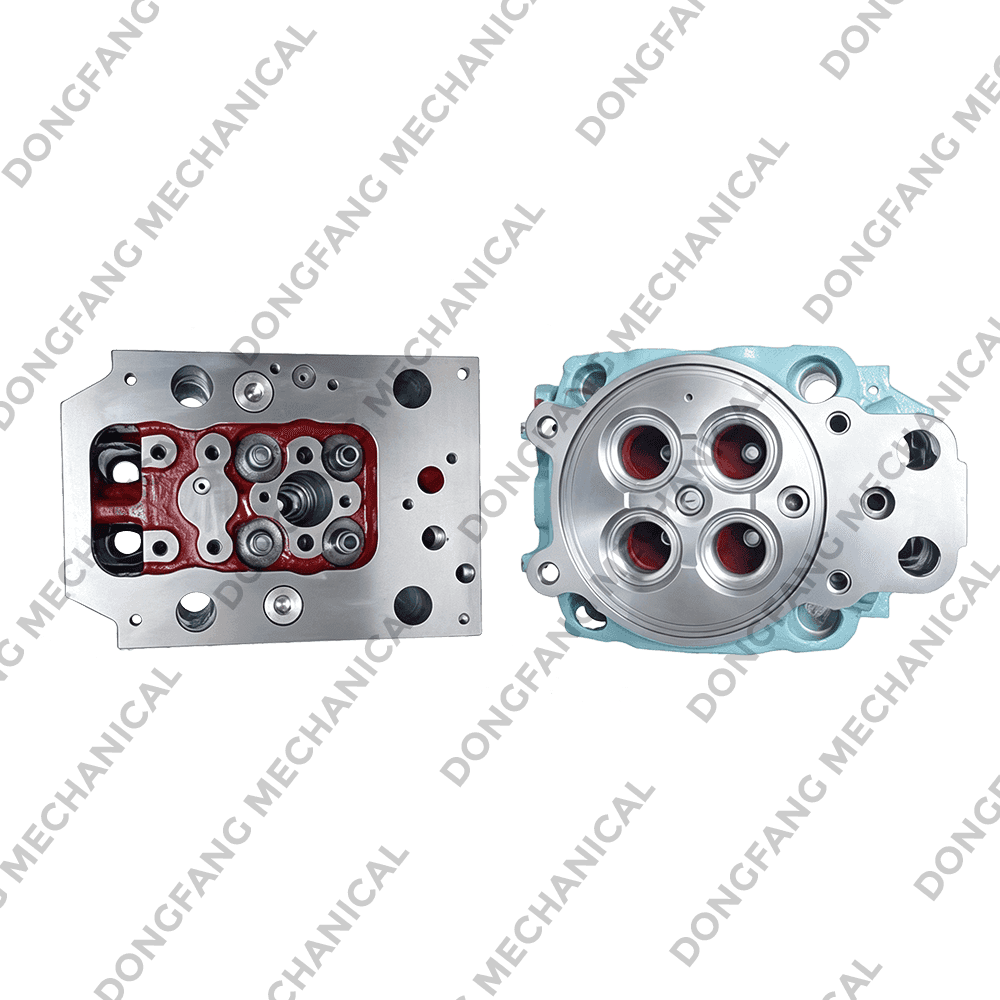
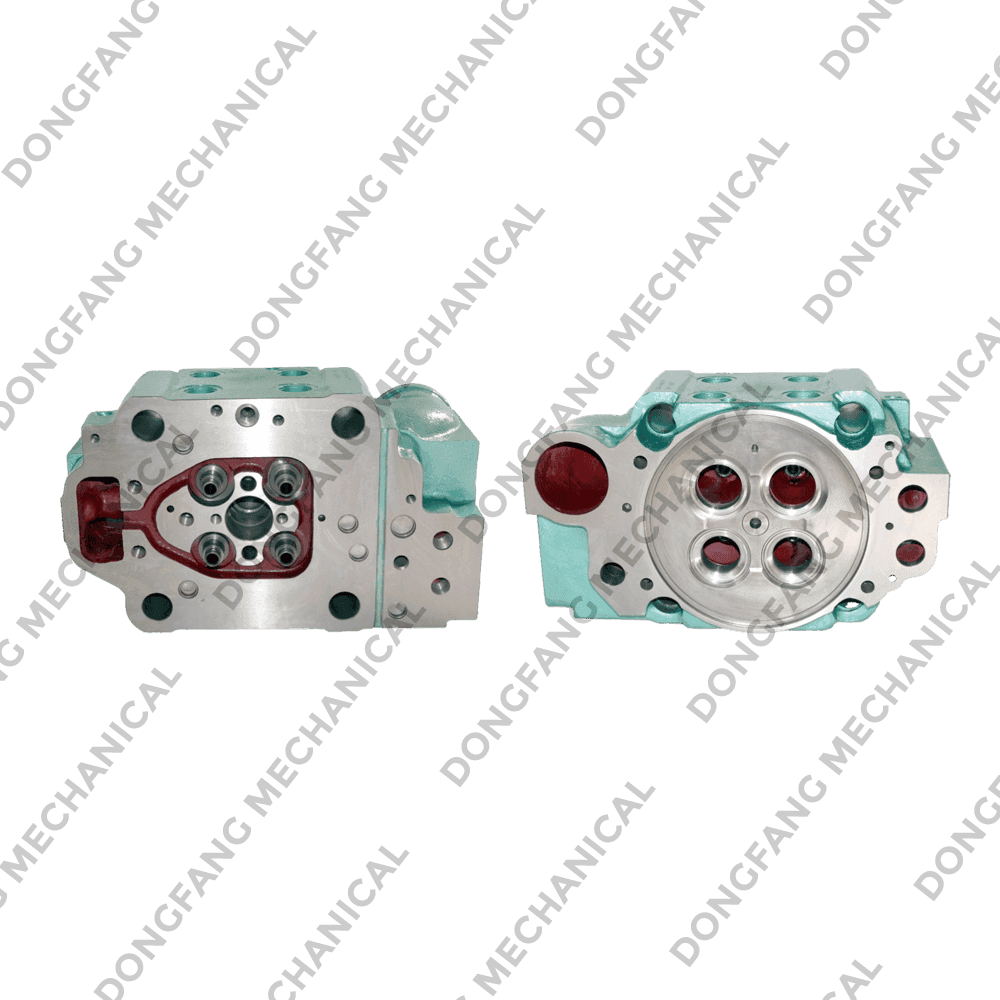
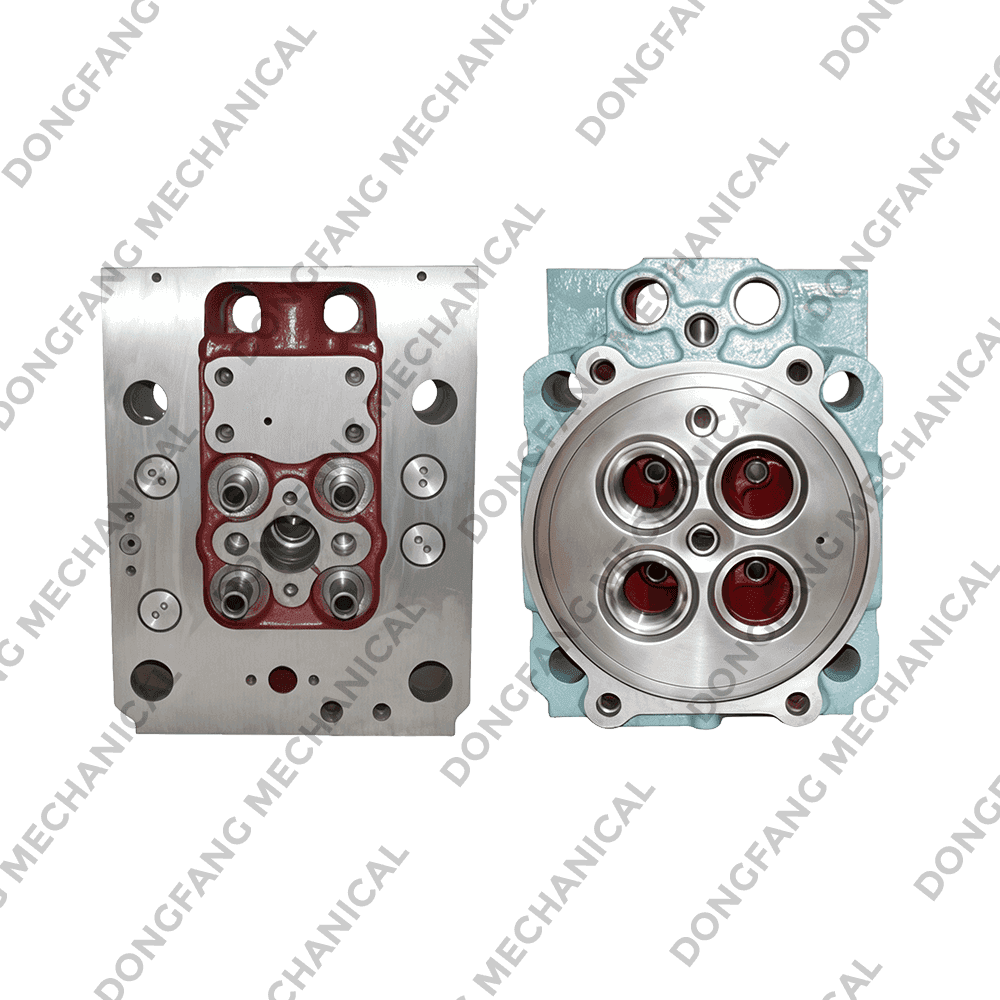
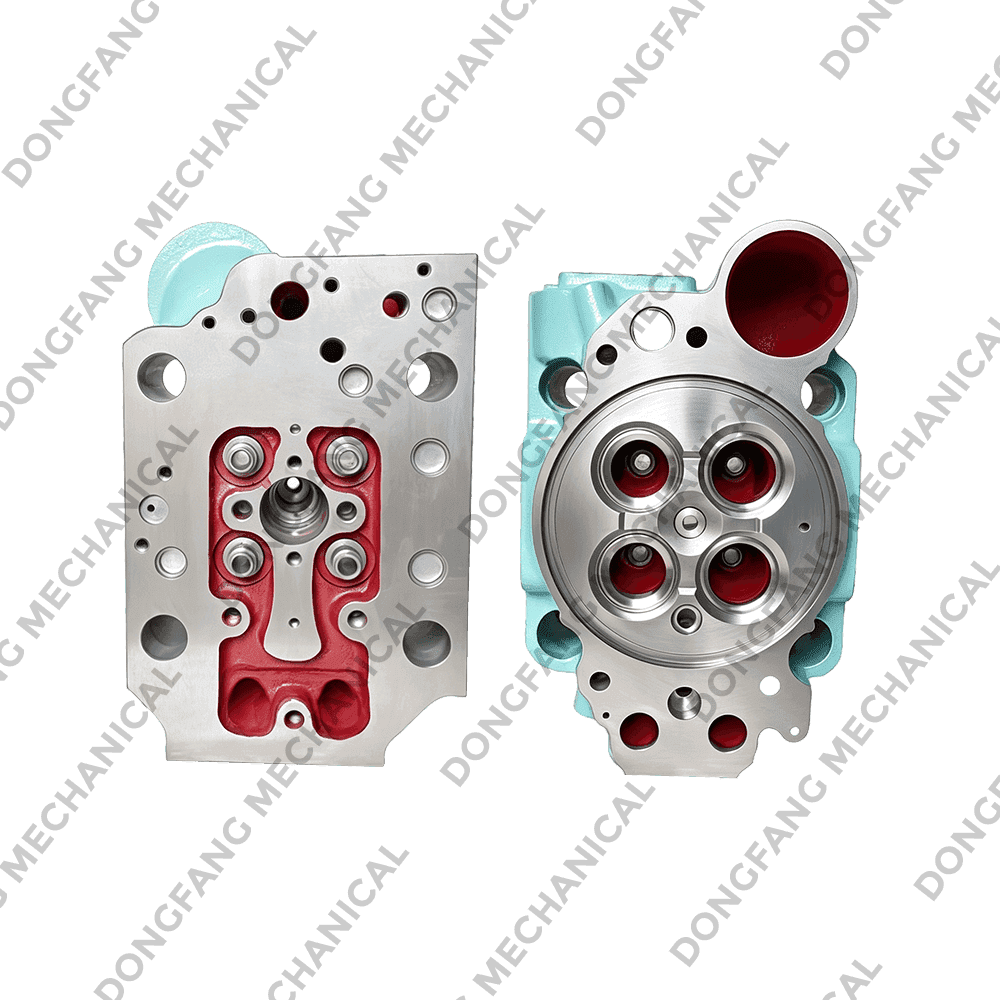
A fishing vessel comes back to port with blue exhaust smoke, a coolant level that keeps dropping, and an engine that needs longer cranking before it fires. The owner asks whether to repair, rebuild, ...
READ MORE
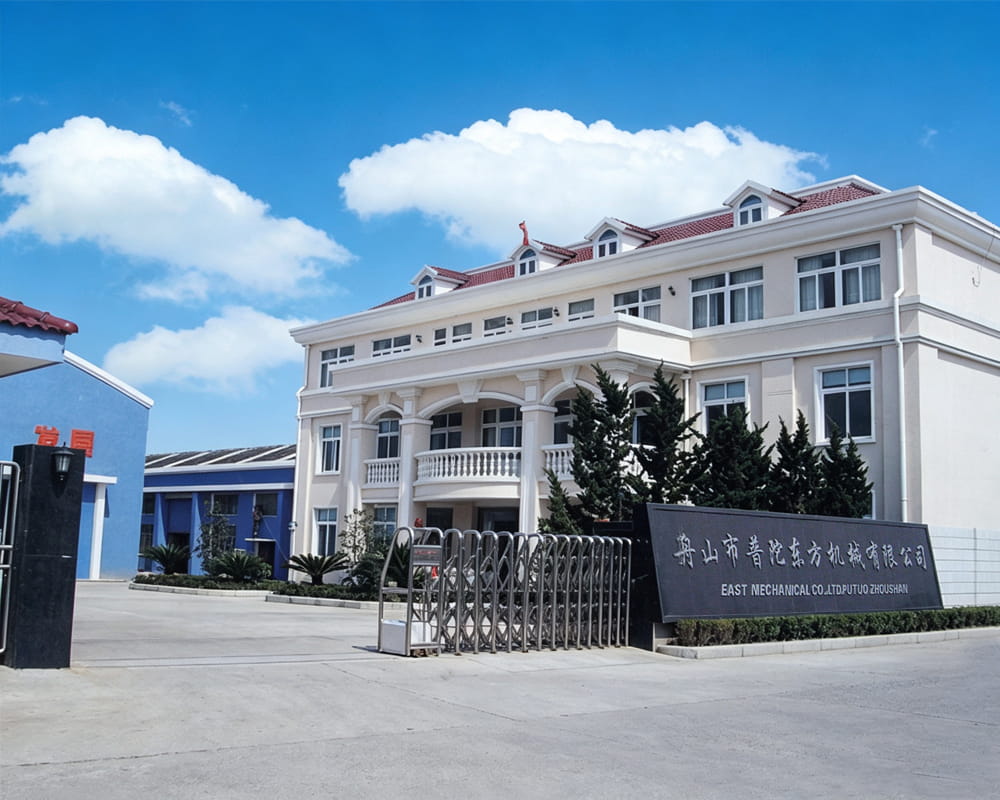
ZHOUSHAN PUTUO DONGFANG MACHINERY CO., LTD.
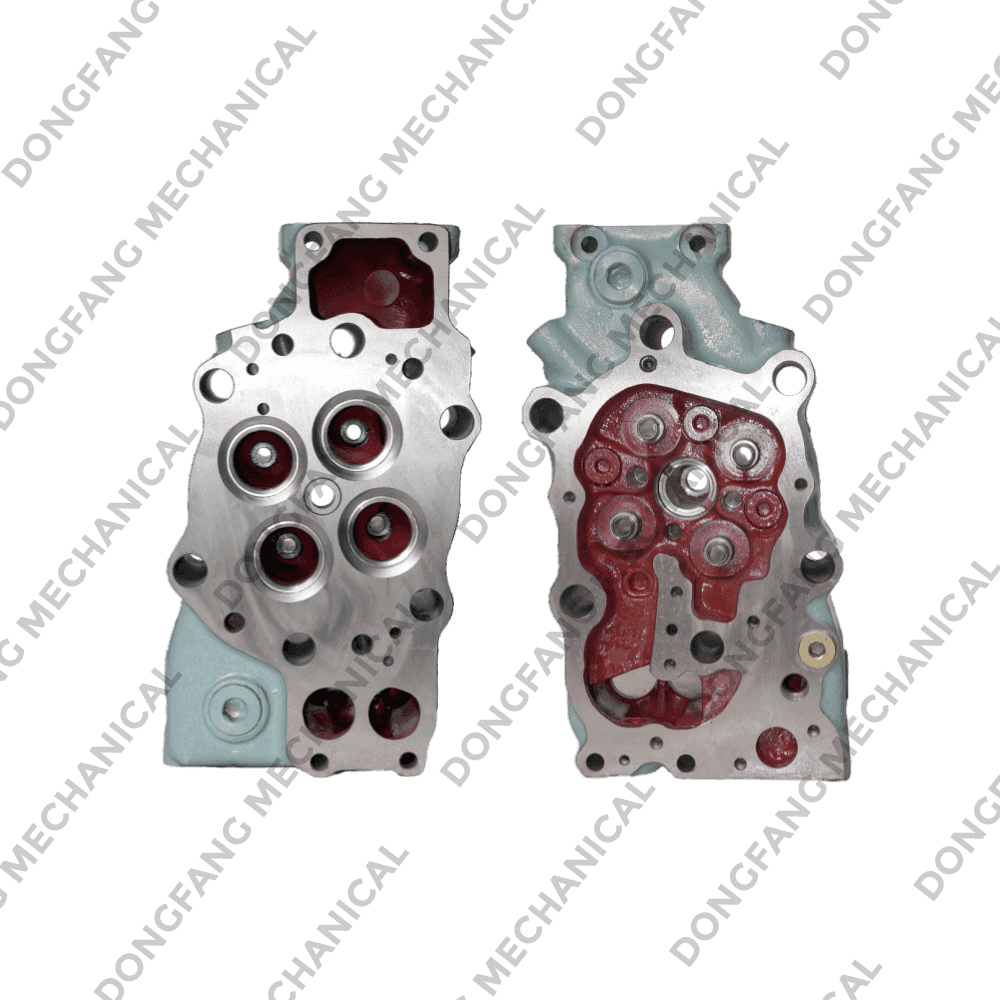
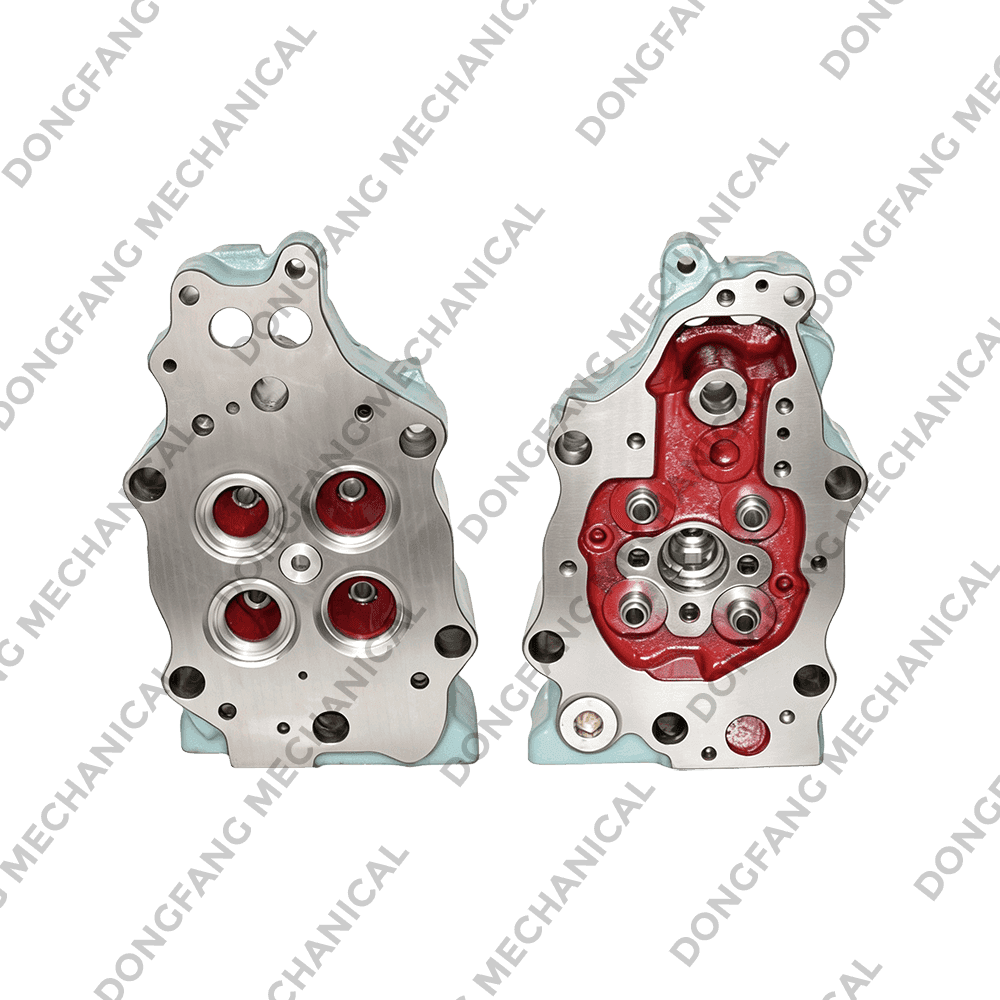
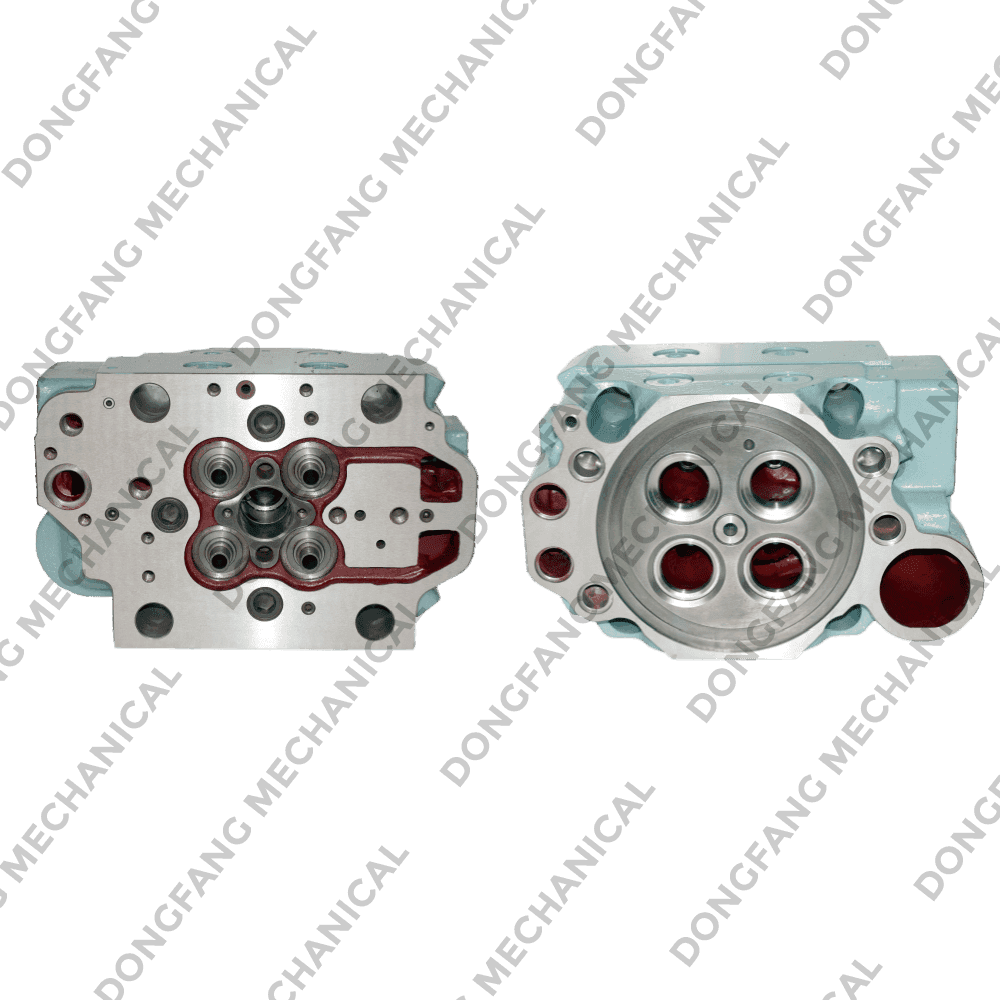
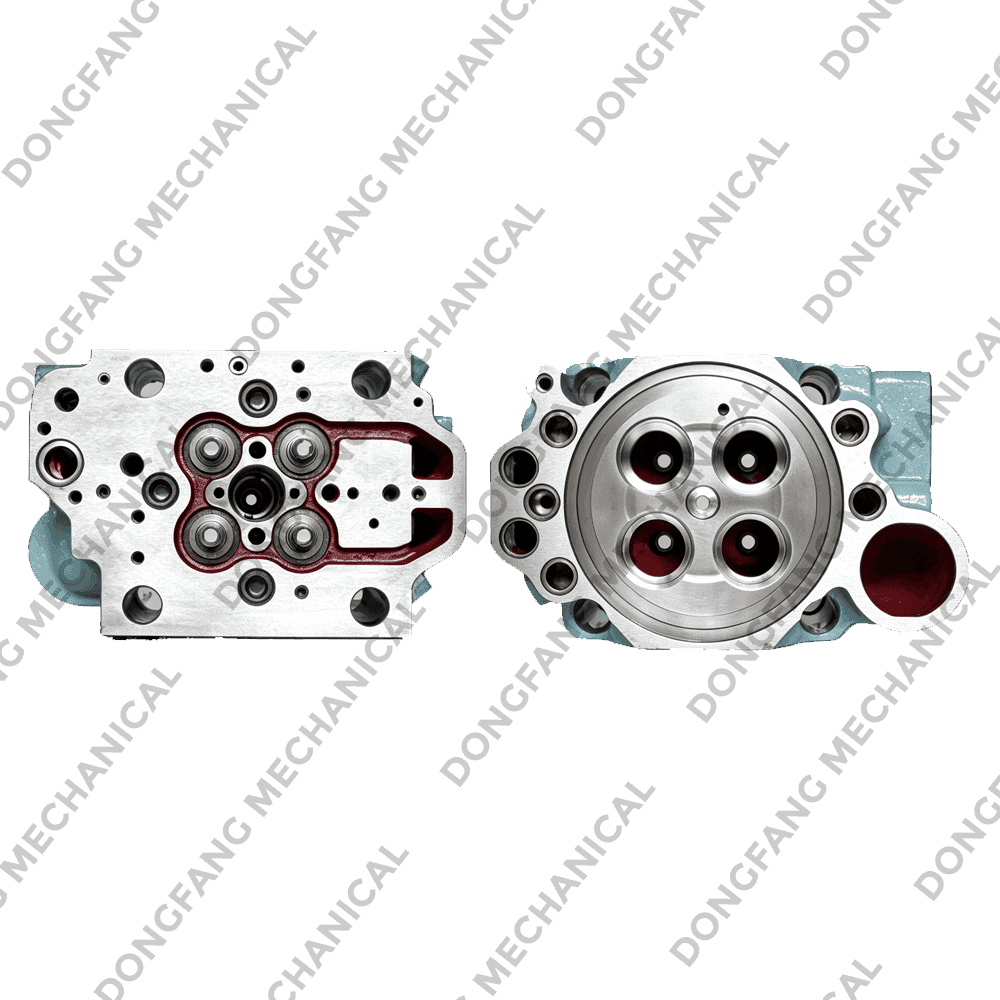
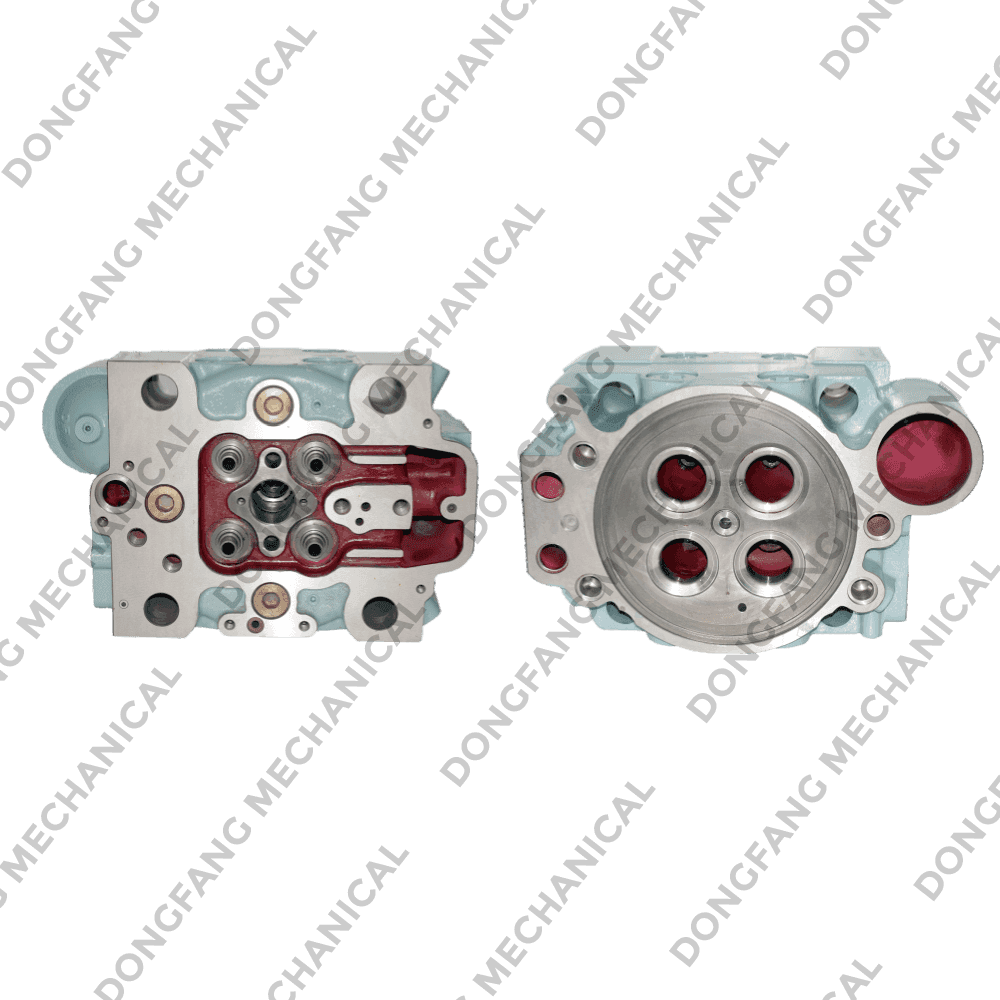
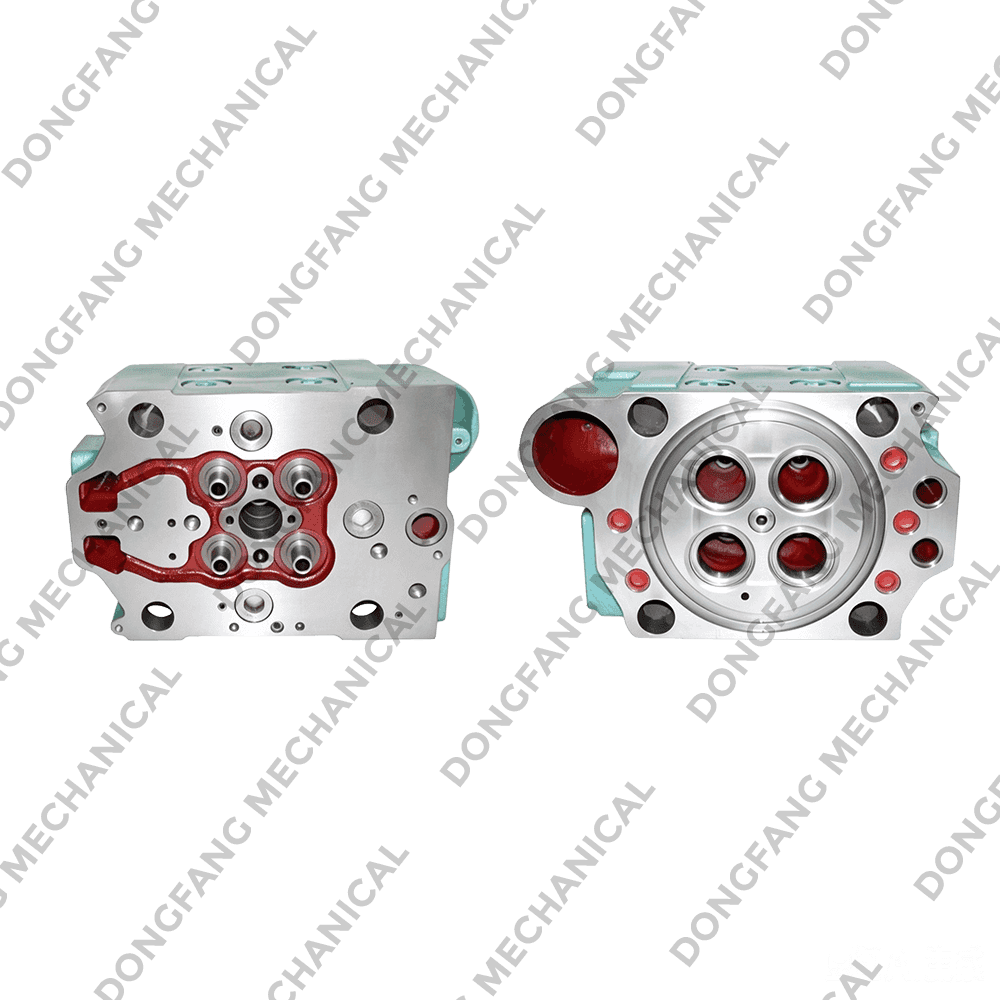
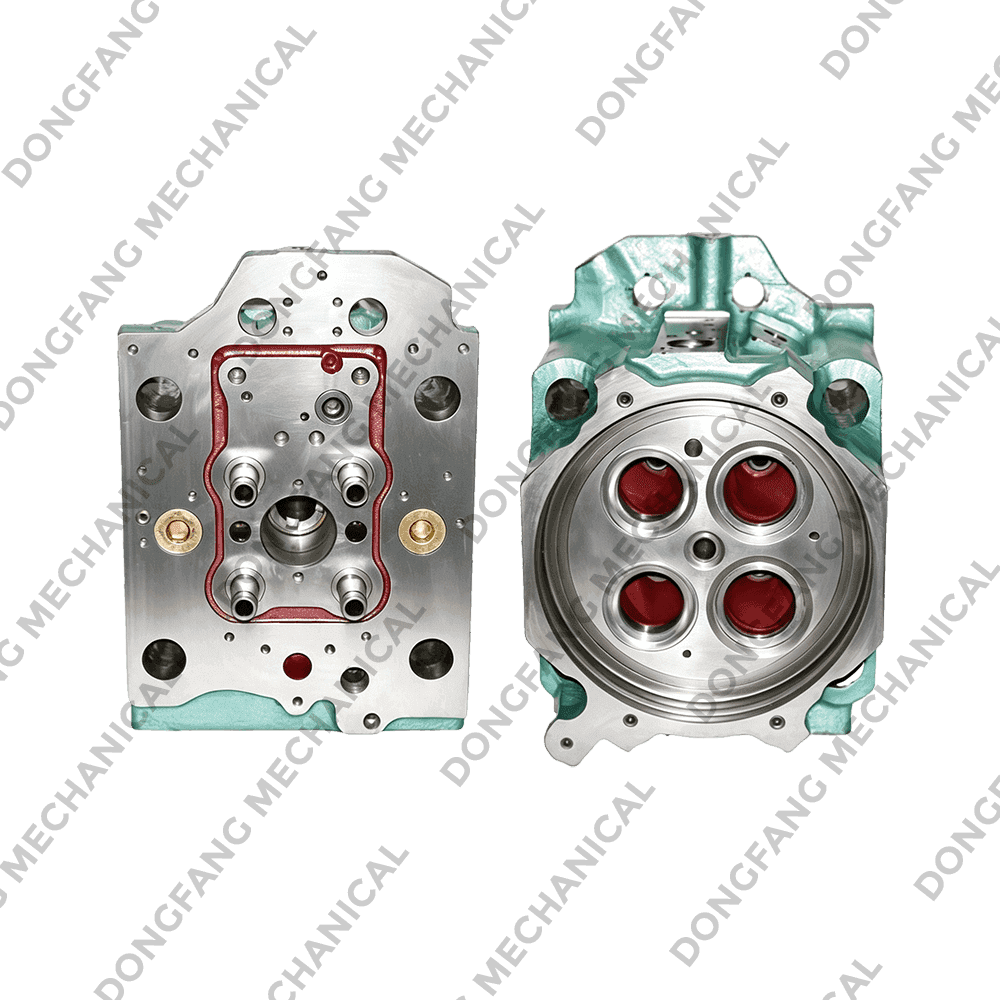
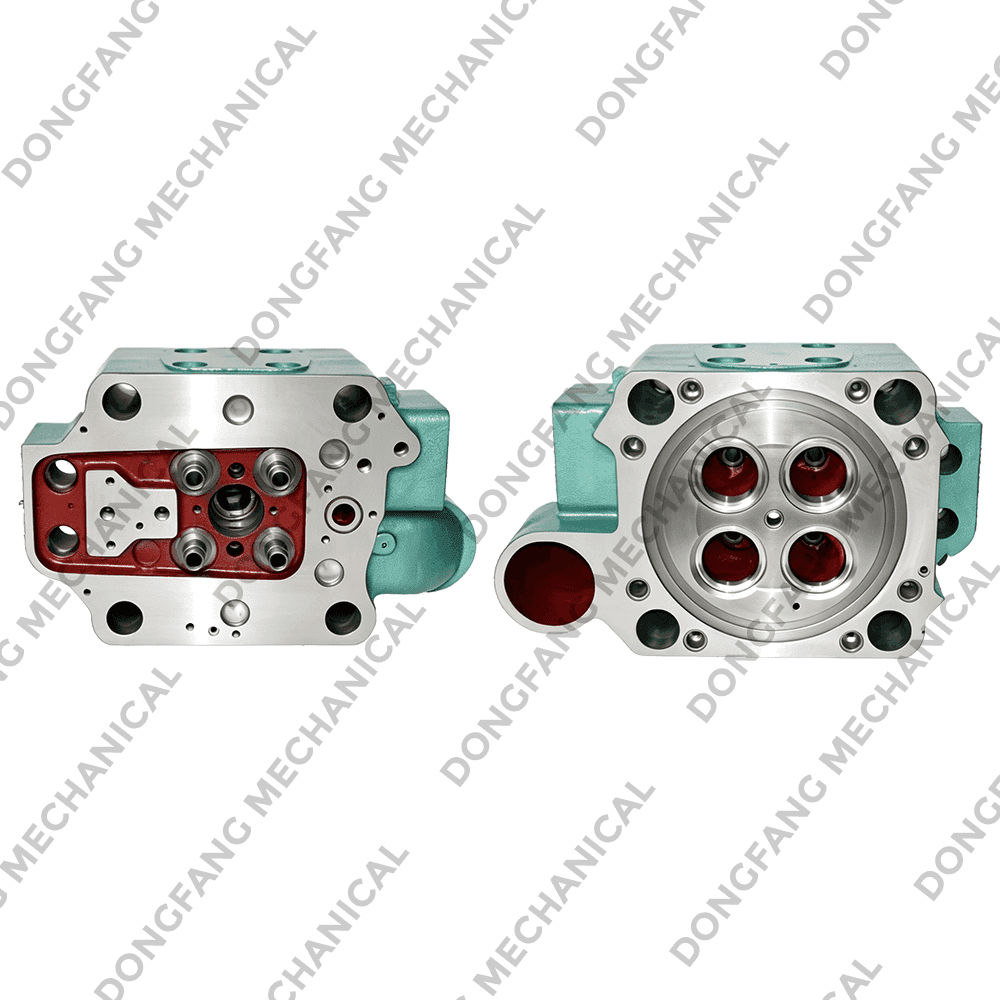
Zhoushan Putuo Dongfang Machinery Co., Ltd. is a China Marine Diesel Engine Cylinder Head Manufacturer and Marine Cylinder Head Factory, located in the Shenjiamen Pingyang Industrial Zone, a well-known fishing port area. It faces the famous Putuo Mountain across the sea, and enjoys convenient land, sea, and air transportation.
The company is one of the earliest local factories engaged in the development, research, manufacturing, and import of diesel engine accessories. With over 20 years of experience in producing and importing accessories, the company boasts a team of experienced, highly skilled professionals with advanced management expertise in mechanical engineering.
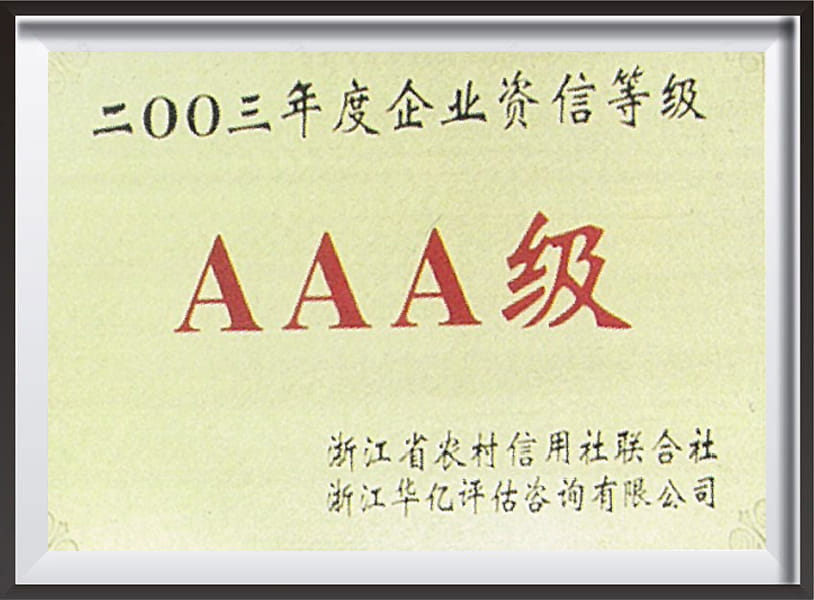
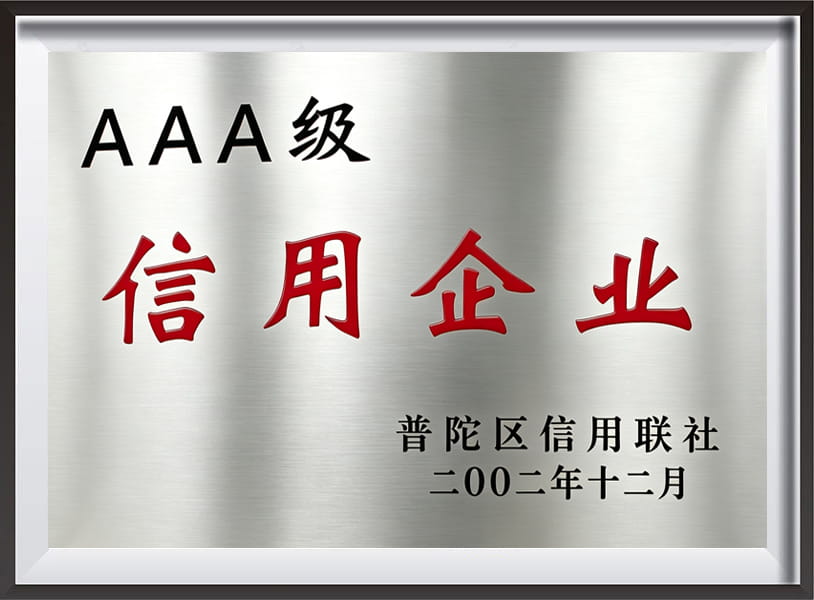
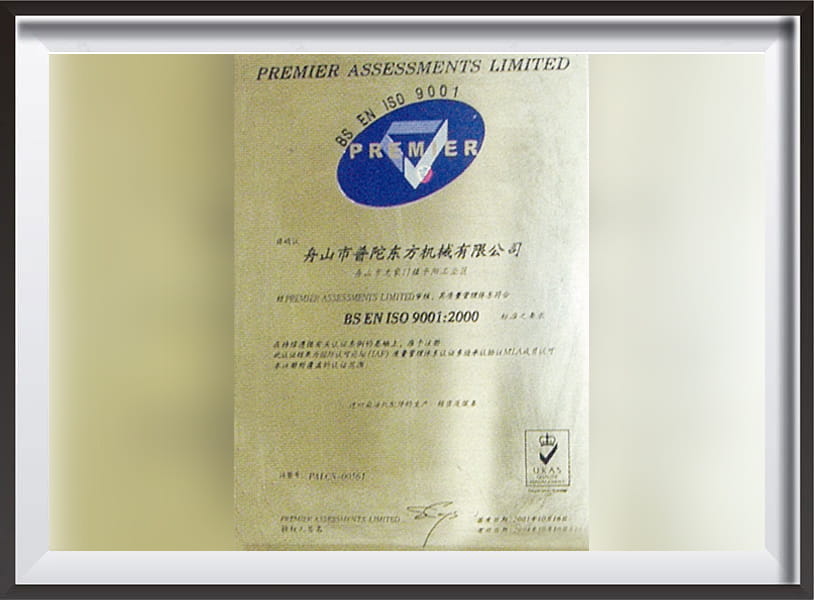
The company passed the ISO 9001 Quality Management System certification in 2001 and has been rated as an AAA-class enterprise for three consecutive years. After decades of development, it now covers an area of over 8000 square meters and produces more than 5,000 sets annually. Equipped with advanced facilities and strong production capabilities, our main products include cylinder heads, cylinder liners. Marine Cylinder Head are widely used in imported marine diesel engines. With stable quality and excellent service, we have established good cooperative relationships with major shipowners and dealers across various regions.
Oriental adheres to the business spirit of integrity, pragmatism, and continuous improvement. We uphold the principle of "Quality First, Reasonable Prices, and Dedicated Service" and look forward to creating a brighter future together with our customers!
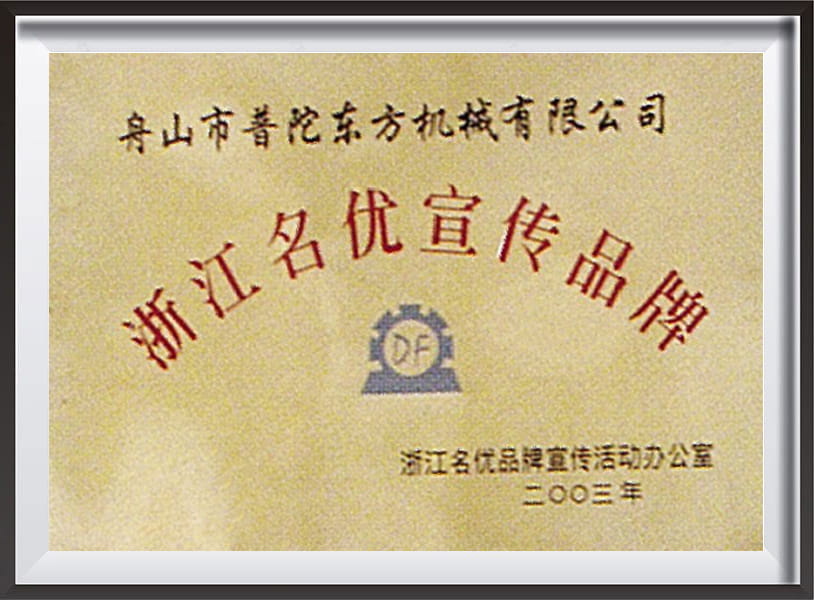
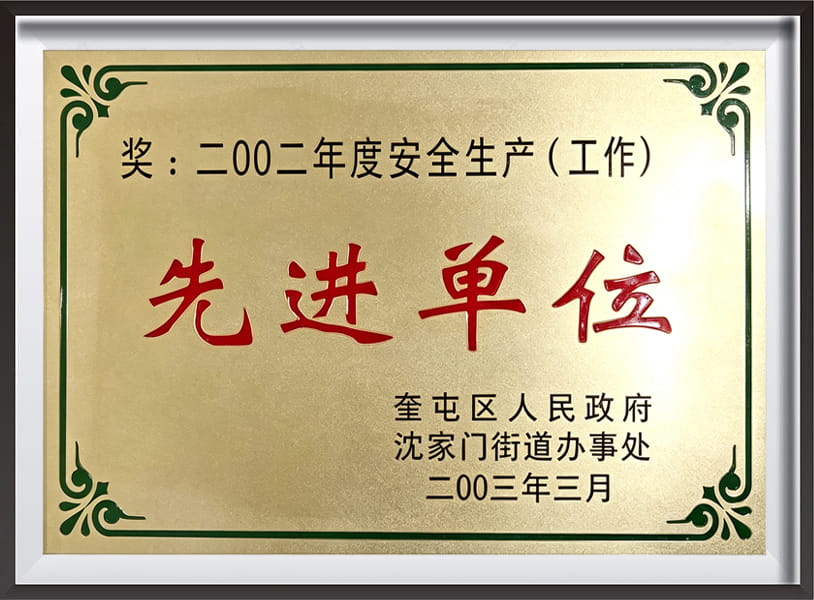
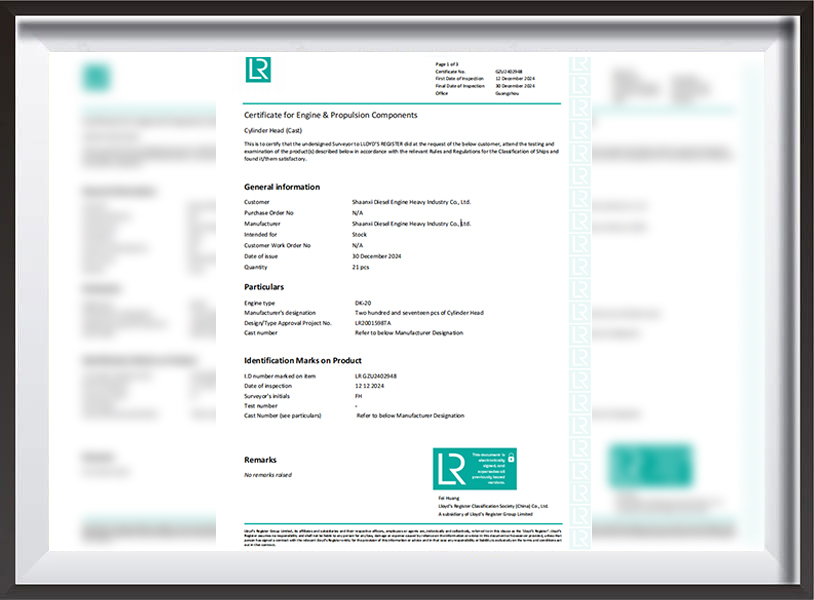
CERTIFICATE OF HONOR
LATEST NEWS
-
-
Your vessel is alongside in Piraeus, the chief engineer reports low compression on number three cylinder, and the next scheduled cargo loading is in four days. The immediate question is not whether a...
READ MORE -
A cracked head or a dropped valve on a working boat is a downtime problem long before it becomes a spare parts problem. Once the engine stops, the only question that matters is whether a compatible r...
READ MORE -
A chief engineer on a tugboat in Southeast Asia faced a familiar problem: a cracked cylinder head on a MAN 8L23/30 auxiliary engine. The vessel had a charter to fulfill in four days. A factory-origin...
READ MORE
INDUSTRY KNOWLEDGE
What a Marine Diesel Engine Cylinder Head Is Built to Do
A marine diesel engine cylinder head manufacturer produces one of the most demanding components in a vessel's propulsion system: the sealed chamber that withstands repeated combustion pressure, high thermal cycling, and constant exposure to seawater-cooled environments. The cylinder head must maintain a precise seal against the cylinder liner and piston assembly while housing valve seats, injector bores, and cooling passages that all need to hold tight dimensional tolerances over thousands of operating hours. Because marine engines run for extended periods under continuous load, any inconsistency in casting density, machining accuracy, or valve seat alignment can lead to compression loss, coolant leakage, or premature valve failure at sea, where replacement parts are far less accessible than on land.
The direct takeaway for vessel operators and procurement teams is that cylinder head sourcing decisions should rest on measurable factors: material integrity, machining precision, thermal fatigue resistance, and consistency in valve seat geometry. This is exactly why working with a dependable marine diesel engine cylinder head factory matters more than comparing catalog specifications alone. This article reviews measured performance data, dimensional trends, and material comparisons to give a clear, practical basis for evaluating cylinder head quality and supplier reliability.
Core Quality Metrics Across Cylinder Head Configurations
When evaluating cylinder heads produced by a marine diesel spare parts manufacturer China buyers typically rely on, five metrics matter most: casting density, machining precision, valve seat alignment accuracy, thermal fatigue resistance, and coolant passage integrity. The horizontal bar chart below scores two common production approaches against these metrics on a 0-100 index built from typical field performance ranges: a conventional sand-cast cylinder head and a precision CNC-machined cylinder head. The CNC-machined configuration scores highest on machining precision and valve seat alignment, since automated toolpaths remove material with far tighter repeatability than manual finishing, while both approaches remain comparable on coolant passage integrity when core-forming processes are well controlled.
This comparison shows that CNC-machined cylinder heads extend their advantage mainly in precision and valve seat alignment, while casting density remains largely dependent on the foundry's own melt quality control rather than the finishing method chosen afterward. Understanding this profile helps fleet operators match cylinder head sourcing to engine model, duty cycle, and expected service interval.
Thermal Stability Across Extended Operating Hours
A key indicator of cylinder head quality is how well the component maintains dimensional stability under sustained thermal cycling once it is installed and running. The line chart below tracks a relative structural stability index across five stages of continuous operating hours, from an early 2,000 hours up to 20,000 hours in a typical mid-speed marine diesel application. A gradual, controlled decline is expected as the metal experiences normal thermal fatigue from repeated heating and cooling cycles, but the trend should remain smooth rather than dropping sharply at any single stage, since a sudden decline would point to residual casting stress or an inadequate stress-relief process rather than routine wear.
The stability index declines from roughly 99% at 2,000 operating hours to about 83% at 20,000 hours, a gradual pattern that stays within acceptable performance for a well-manufactured component before the next scheduled overhaul. This kind of predictable degradation curve is exactly why consistent, controlled casting and stress-relief processes matter: a properly manufactured cylinder head from a reliable China marine cylinder head manufacturer ages in this smooth, expected way rather than developing cracks or warping unpredictably mid-voyage.
Where Cylinder Heads Are Commonly Deployed by Vessel Type
The application spread of marine diesel engine cylinder heads reflects the wide range of vessel types that depend on dependable engine performance. The vertical bar chart below shows a representative usage breakdown across common vessel categories, based on aggregated field usage patterns. Fishing vessels lead the distribution, followed by cargo and bulk carriers, tugboats and workboats, and passenger or ferry vessels.
Fishing vessels account for roughly 32% of typical deployment, reflecting the dense concentration of coastal and offshore fishing fleets that rely on consistent engine uptime during long voyages. Cargo and bulk carriers follow closely, since these vessels operate on tight scheduling windows where unplanned cylinder head replacement can directly disrupt delivery timelines.
Cast Iron Versus Compacted Graphite Iron Cylinder Heads
A radar chart helps visualize the trade-off between a standard gray cast iron cylinder head and a compacted graphite iron (CGI) cylinder head across multiple dimensions simultaneously. The chart below compares both across thermal fatigue resistance, machinability, tensile strength, corrosion resistance, and manufacturing cost efficiency. The compacted graphite iron head extends further on thermal fatigue resistance and tensile strength, since its microstructure resists crack propagation under repeated heat cycling more effectively, while the gray cast iron head extends further on machinability and manufacturing cost efficiency, since it is easier and faster to machine into finished form.
Neither material profile covers every dimension, reinforcing why material selection should be driven by engine duty cycle and thermal loading rather than assuming one option is universally superior. High-load, continuous-duty engines favor compacted graphite iron, while moderately loaded applications with tighter budget constraints may still perform well with standard gray cast iron.
Practical Selection Guidance by Application
Choosing the right marine diesel engine cylinder head starts with identifying engine model, duty cycle, and typical operating environment. The table below summarizes practical guidance across common scenarios drawn from field experience with a marine engine spare parts factory China buyers commonly source from.
Scenario-Based Selection Reference
| Application | Suitable Configuration | Reason |
|---|---|---|
| Continuous-duty cargo vessel engines | Compacted Graphite Iron Cylinder Head | Superior thermal fatigue resistance under sustained load |
| Coastal fishing vessel engines | Gray Cast Iron or CGI Cylinder Head | Balanced durability and machining turnaround |
| Tugboat and workboat engines | Gray Cast Iron Cylinder Head | Cost-efficient machining for frequent maintenance cycles |
| High-load bulk carrier engines | Compacted Graphite Iron Cylinder Head | Higher tensile strength under continuous thermal cycling |
Before placing a marine diesel engine cylinder head into regular service, a few additional checks help support consistent performance:
- Confirm casting material grade matches the original engine manufacturer specification.
- Verify valve seat and guide dimensions against the engine's service manual before installation.
- Check coolant passage clearances to prevent overheating during extended operation.
- Inspect gasket sealing surfaces for flatness that could affect combustion sealing.
- Schedule periodic torque and compression checks to maintain reliable engine output over time.
Manufacturing Consistency Behind Dependable Cylinder Head Performance
The predictable stability curve discussed earlier depends on consistent manufacturing at the foundry and machining stage, including controlled melt chemistry, proper stress-relief heat treatment, and precise CNC finishing of valve seats and mating surfaces. Variation in any of these steps can shift both dimensional precision and how evenly the cylinder head performs once installed, which is why tight process control matters throughout production at a dependable marine diesel engine cylinder head manufacturer. Automated machining and in-process precision testing help keep each cylinder head performing within tight tolerances across its service life, supporting the reliability trends referenced throughout this article.
Standard quality checkpoints such as pressure testing, valve seat concentricity verification, and dimensional inspection support the performance trends shown earlier. For procurement teams sourcing cylinder heads and related spare parts at scale, confirming these quality checkpoints with a supplier is often as valuable as reviewing published specifications alone.
About Zhoushan Putuo Dongfang Machinery Co., Ltd.
Zhoushan Putuo Dongfang Machinery Co., Ltd. is located in the Shenjiamen Pingyang Industrial Zone, a well-known fishing port area. It faces the famous Putuo Mountain across the sea, and enjoys convenient land, sea, and air transportation. This location places the company at the center of a region where marine engine maintenance and spare parts supply are part of daily operations, giving practical, field-tested insight into what fishing fleets, cargo operators, and workboat owners need from a reliable cylinder head.
As a marine diesel spare parts manufacturer China operators can rely on, the company focuses on producing precision-machined cylinder heads and related components that meet the dimensional accuracy and material integrity standards required for continuous marine service. Its position within a major fishing port area supports fast turnaround for regional vessel owners while maintaining the consistent manufacturing controls needed to serve customers across broader shipping and fishing industries.
Frequently Asked Questions
Q1: Why does casting quality matter more than surface finish alone?
A1: A cylinder head with poor internal casting density can develop micro-porosity that leads to coolant leaks or cracking under thermal cycling, even if the exterior finish looks acceptable, so internal integrity checks matter as much as visible machining quality.
Q2: How often should a cylinder head be inspected during normal service?
A2: Inspection intervals should follow tracked operating hours and observed compression trends, since structural stability typically declines gradually rather than at one fixed universal interval across all engine types.
Q3: Is compacted graphite iron always the better material choice?
A3: Not necessarily; CGI offers stronger thermal fatigue resistance and tensile strength for continuous, high-load engines, while gray cast iron can still be a practical choice for engines with moderate duty cycles and more frequent maintenance schedules.
Q4: What causes uneven sealing across a newly installed cylinder head?
A4: Warped mating surfaces, inconsistent torque application, or gasket sealing surface irregularities are common causes, which is why flatness checks and calibrated torque procedures matter during installation.
Q5: What manufacturing factors most affect cylinder head reliability?
A5: Melt chemistry control, stress-relief heat treatment, and CNC machining precision are key factors, supported by process checks such as pressure testing and valve seat concentricity verification during production at a qualified marine diesel engine cylinder head factory.

Get in Touch
Your email address will not be published. Required fields are marked *
contact us
ARE YOU INTERESTED IN ANY
OF OUR PRODUCTS?
Price is favorable.Welcome to inquire.
Company Address
Pingyang Industrial Zone, Shenjiamen, Zhoushan City, Zhejiang Province, China.
Tel:
+86-15957856920 Chancy
E-mail:
chancyliu@vip.163.com
-
Zhoushan Putuo Oriental Machinery, with twenty years of focus on imported marine diesel engine core components. Building good karma through stable quality, and sailing far with dedicated service.
 Copyright © Zhoushan Putuo Dongfang Machinery Co., Ltd. Marine Diesel Engine Cylinder Head Manufacturer All Rights Reserved.
